The Carbon Footprint of Recycled Aluminum: How to balance performance and ESG?
In today's world where carbon neutrality and supply chain transparency are the norm, recycled aluminum has become one of the preferred materials for gravity casting due to its low carbon footprint. Compared to primary aluminum (produced through alumina electrolysis), recycled aluminum can reduce energy consumption by 3–5% and carbon emissions by 80–95%, which is of great significance for companies' ESG and EU CBAM compliance. However, the key to simultaneously maintaining mechanical properties and stable mass production lies in "source control + process optimization".
The Carbon Footprint Challenge of Primary Aluminum
Aluminum is widely used in industries such as automotive, aerospace, and electronics due to its lightweight, corrosion resistance, and excellent thermal conductivity. However, the traditional production process of primary aluminum is energy-intensive. From mining bauxite and refining alumina to electrolytic reduction into primary aluminum, each step consumes a significant amount of electricity, resulting in a relatively high carbon footprint for primary aluminum. Faced with increasingly stringent environmental regulations and customer demands for green supply chains, finding more environmentally friendly alternatives is imperative.
Recycled Aluminum: A Green Choice for Significantly Reducing Carbon Footprint
Recycled aluminum, also known as secondary aluminum or recycled aluminum, is an aluminum alloy made from waste aluminum products (such as scrapped car parts, packaging containers, building materials, etc.) through recycling, sorting, smelting, and refining. Its most significant advantage is that it can greatly reduce energy consumption and carbon footprint.
Studies show that using recycled aluminum requires only about 5% of the energy needed to produce primary aluminum, which means a significant reduction in carbon emissions. Therefore, actively adopting recycled aluminum is not only fulfilling corporate social responsibility but also an inevitable choice in response to the global green transformation trend.
Performance Myth: Recycling Does Not Equal Quality Compromise
Many people worry that recycled aluminum will suffer from compromised performance, but the opposite is true. Modern aluminum recycling technology has reached an extremely high level:
- Purity Control: Through advanced smelting technology, the purity of recycled aluminum can reach over 99.7%, which is comparable to that of primary aluminum.
- Alloy Design: Precise composition control ensures that mechanical properties meet the requirements of various applications.
- Consistent Quality: A comprehensive raw material grading system has been established to ensure the consistency of quality in each batch of recycled aluminum.
Ming Ming Aluminum's experience has proven that gravity-cast products using recycled aluminum fully meet or even surpass the performance standards of virgin aluminum products in key indicators such as tensile strength and elongation. With 95% energy savings and nearly 90% carbon emission reductions, recycled aluminum is not only crucial for the aluminum industry to reduce its environmental burden but also a vital tool for companies to demonstrate social responsibility and market competitiveness in the ESG era. Promoting the widespread adoption and innovation of recycled aluminum, while balancing performance and environmental protection, will be the inevitable path for the sustainable development of the aluminum industry in the future.
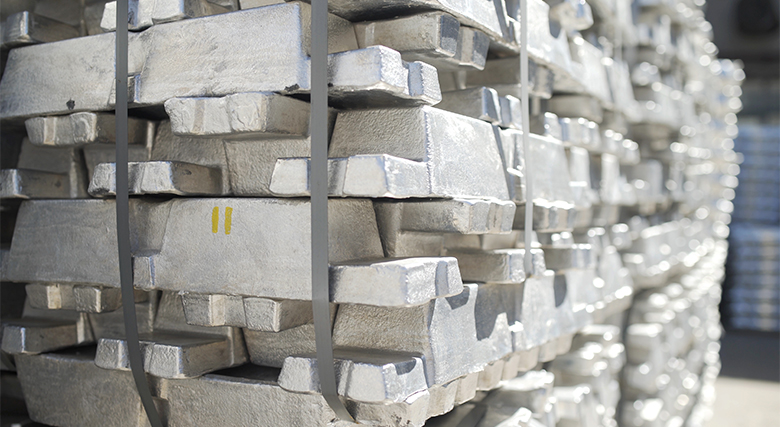
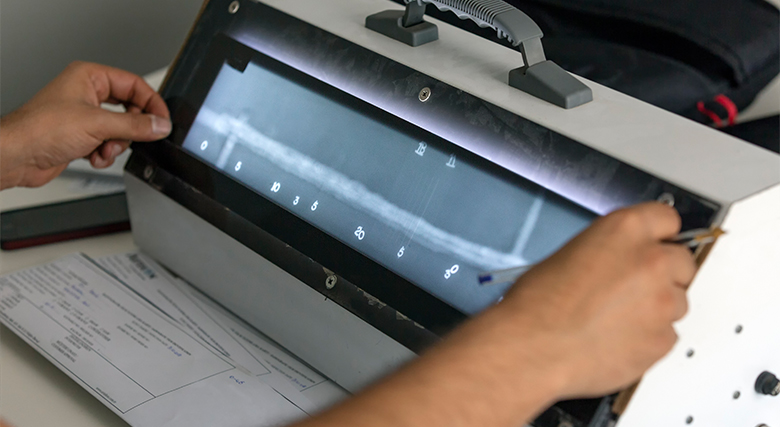
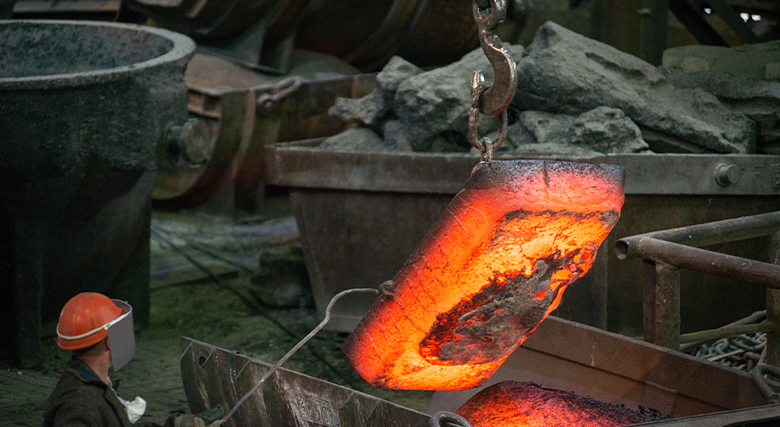
Ming Ming employs a smelting ratio of 65:35 or 50:50 weight percentage of primary aluminum to recycled aluminum to reduce energy consumption and carbon emissions in primary aluminum electrolysis production. Recycled aluminum of various materials is first classified and stored centrally, and only used for smelting the same material at a time to avoid unnecessary material contamination. After the primary and recycled aluminum are smelted, the molten aluminum in each furnace undergoes spectrophotometric material analysis and degassing and slag removal to ensure its quality. Furthermore, Ming Ming has K-mold testing equipment for specific gravity, vacuum testing, and other physical properties to ensure quality control. Ming Ming also continuously monitors the A356 tensile test results under recycled aluminum usage (all meeting customer mechanical property requirements).